63/37 vs 60/40 Solder: The Practical Difference, Side by Side
Opening Introduction
Quick answer:63/37 and 60/40 are both tin-lead solders that melt around 183°C, but they behave differently on the iron. 63/37 is eutectic, so it flips from solid to liquid at a single temperature with no in-between “mushy” stage — easier to hand-solder and far less likely to throw a cold joint. 60/40 has a ~7°C plastic range (183–190°C), so a joint can shift and crack while it sets. For hand soldering and rework, grab 63/37; 60/40 is fine for general work and costs a little less. One thing both share: neither is RoHS-compliant — they’re both lead-based.
If you’ve stood in the solder aisle wondering whether the extra tin in 63/37 is worth the few cents, you’re not alone. The two alloys look identical on the spool and the specs overlap just enough to be confusing. They’re not the same thing, though, and the difference shows up the moment you touch the iron.
What "eutectic" actually means
This is the whole ballgame, so it’s worth getting right.
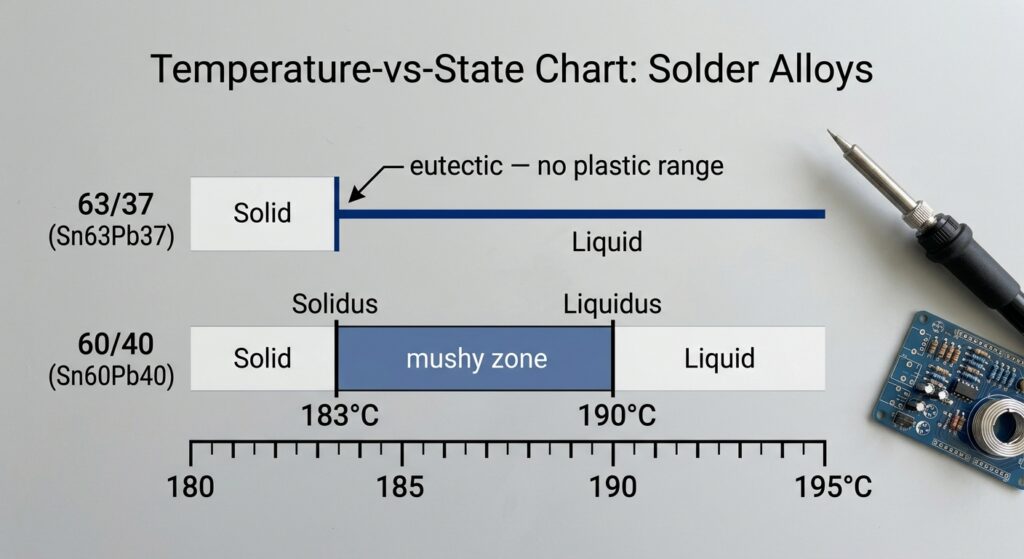
A pure metal melts at one exact temperature. Mix two metals and you usually get a range: the alloy starts softening at the solidus temperature and only becomes fully liquid at the liquidus temperature. In between, it’s a paste — part solid, part liquid. That in-between zone is called the plastic (or “mushy”) range, and it’s where joints get disturbed.
A eutectic alloy is the exception: it has a single, sharp melting point with no plastic range. Real eutectic tin-lead is 61.9% Sn / 38.1% Pb at exactly 183°C. Commercial 63/37 sits close enough that it behaves as eutectic in practice — it goes solid→liquid in one clean step.
60/40 is not eutectic. Its solidus is 183°C and its liquidus is ~190°C, leaving a ~7°C window where it’s half-melted.
63/37 vs 60/40 at a glance
| Property | 60/40 (Sn60Pb40) | 63/37 (Sn63Pb37) |
|---|---|---|
| Tin / lead | 60% / 40% | 63% / 37% |
| Eutectic? | No | Yes (effectively) |
| Melting point | 183–190°C (range) | 183°C (sharp) |
| Plastic range | ~7°C (mushy) | None |
| Fluidity on the iron | Good | Better / wets faster |
| Cold-joint risk | Slightly higher | Lower |
| Relative cost | Lower | Slightly higher (more tin) |
| Best for | General / through-hole / dip | Hand soldering, rework, precision |
| RoHS-compliant? | No (contains lead) | No (contains lead) |
Where they're the same
People mix these up for a reason — they share the basics:
- Both are lead-based soft solders. Neither is RoHS-compliant, full stop. If you need lead-free, you’re looking at SAC305 (Sn96.5/Ag3.0/Cu0.5) or similar, not either of these.
- Both start melting at 183°C, so your iron temperature and technique carry over between them.
- Both take rosin-core or acid-core, work in wave soldering and reflow, and form strong, conductive joints when done right.
- Both are easy to find and cheap enough that solder cost is rarely the deciding factor in a project.
Where they actually differ
The mushy zone is the big one. With 60/40, if a part moves, the board flexes, or you pull the iron a beat too early while the joint is still in that 183–190°C paste, you get a disturbed or cold joint — grainy, dull, unreliable. 63/37 skips that stage entirely, so the window for screwing it up is smaller.
Fluidity. Because 63/37 hits liquid cleanly, it wets and flows a touch faster, which means fewer solder bridges between tight pins and a neater fillet.
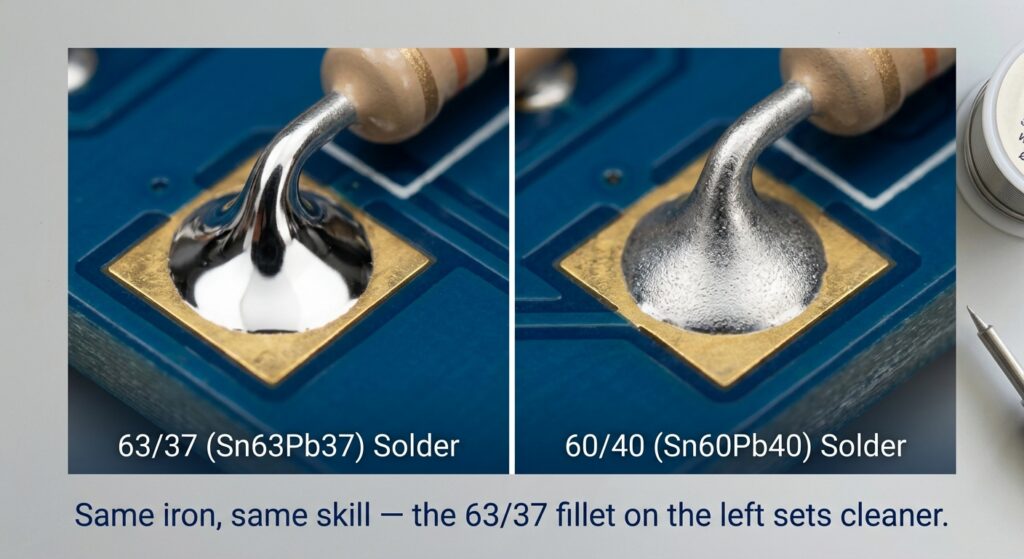
Finish. 63/37 joints tend to look bright and smooth as they set; 60/40 can look slightly duller or grainier because of that partial-solidification texture.
Price. 63/37 carries more tin, so it’s usually a hair more expensive per spool. For most hobbyists the gap is meaningless; for high-volume production it adds up.
Which should you actually use?
If you only keep one spool on the bench, make it 63/37. The eutectic behavior is more forgiving, especially for hand soldering, through-hole rework, and any work where you’re holding the joint while it cools. It’s the alloy most pro bench techs reach for by default.
Reach for 60/40 when:
- You’re doing high-volume dip or wave soldering and the plastic range is actually useful for the process.
- You’re cost-sensitive on a large run and the joints aren’t precision-critical.
- It’s simply what’s in the drawer and the job is straightforward.
Either way, the mechanical strength difference is small enough that it rarely decides a real-world failure. The win with 63/37 is consistency and fewer do-overs.
The RoHS myth (most guides get this wrong)
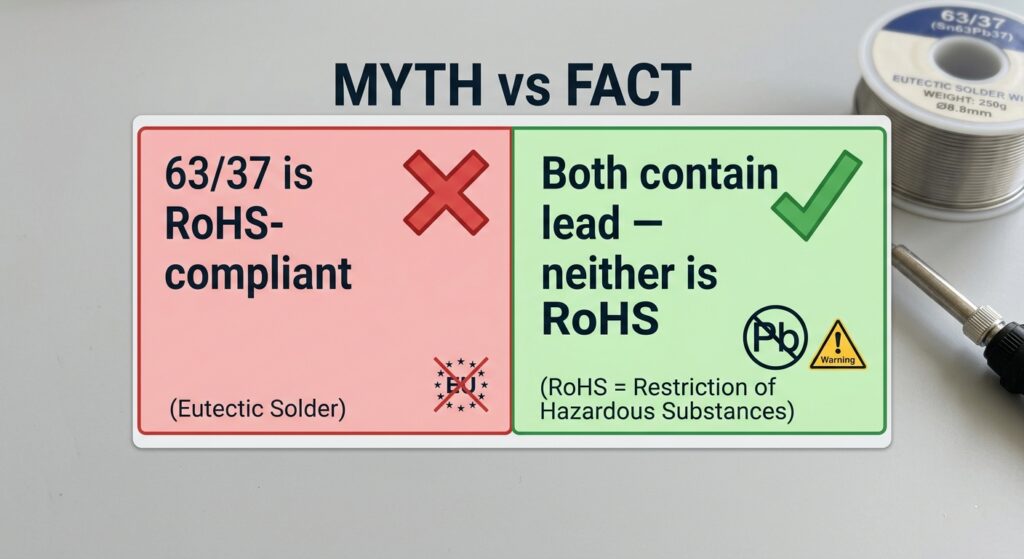
You’ll see articles claim 63/37 is “closer to RoHS-compliant” or safer on regulations. That’s false. RoHS restricts lead outright; an alloy that’s 37% lead is nowhere near compliant. The “safer” move isn’t picking 63/37 over 60/40 — it’s going lead-free (SAC305 and friends) when the product must meet RoHS. 63/37’s only real edge on the regulation front is that it uses slightly less lead, which changes nothing for compliance.
Frequently Asked Questions (FAQ)
A:Is 63/37 solder better than 60/40?
For hand soldering and rework, yes — its eutectic, single-point melt makes cleaner joints with less risk of cold spots. For bulk automated soldering, 60/40 is a common, cost-effective choice. Neither is “stronger” in a way that usually matters.
A:Can I use 60/40 and 63/37 interchangeably?
On the same iron and temperature, yes — both melt near 183°C and form reliable joints. Just expect 60/40 to need a steadier hand during cool-down because of its mushy range. Don’t mix the two alloys in the same joint if you can avoid it.
A:Is 63/37 solder RoHS compliant?
No. It’s roughly 37% lead, and RoHS bans lead in most electronics. For RoHS you need a lead-free alloy like SAC305. 63/37 is easier to work with than 60/40, but it is not the compliant option.
About US
You may also be interested in…

About the Author
Andrew Zhan – R&D Engineer at JKRGLO.com
With over 14 years of R&D engineering experience in the PCB industry, Andrew Zhan brings deep expertise in circuit design optimization and DFM implementation. He focuses on translating complex design requirements into production-ready solutions, driving technical innovation for both prototype and mass production.
Working closely with cross-functional teams and clients, he ensures rigorous quality validation and seamless technical communication across the full project lifecycle. Andrew is committed to delivering reliable, high-performance PCB solutions that consistently exceed customer expectations.
Table of Contents
Still, need help? Contact Us:
Need a PCB or PCBA quote?
Tag:
63-37
PCBA
63 37 solder
PCB